Every decoration method does beautiful work inside its limits. Push past them and you do not get a warning at the design review; you get a failure three sample rounds later. The practical rule is to confirm that each finish is feasible on the actual production method, at production speed and through the logistics chain, before artwork is finalised. This guide covers the limits that matter most on primary packaging: silk-screen, hot stamp and foil, soft-touch and matte finishes, and sleeve or wrap labels.
Silk-screen: cure time and registration
Silk-screen printing puts ink onto the container through a mesh, and it suits bold, graphic artwork on bottles, jars and tubes. Its limits are mostly about process time and precision.
- Cure time. Inks need to cure before the piece is handled, stacked or packed. A schedule that ignores cure time leads to marking and adhesion problems.
- Registration tolerance. Multi-colour artwork needs each colour aligned to the others. Tighter registration is possible, but it costs more and needs slower, more closely monitored runs.
- Curved and tapered surfaces. Artwork that wraps or sits near a seam or shoulder is harder to hold consistently than artwork on a flat panel.
Ask the decorator for a stated registration tolerance in writing, and design artwork so that small shifts do not ruin the look. A thin outline that must sit perfectly inside a fill will show every variation.
Hot stamp and foil: feature size and curves
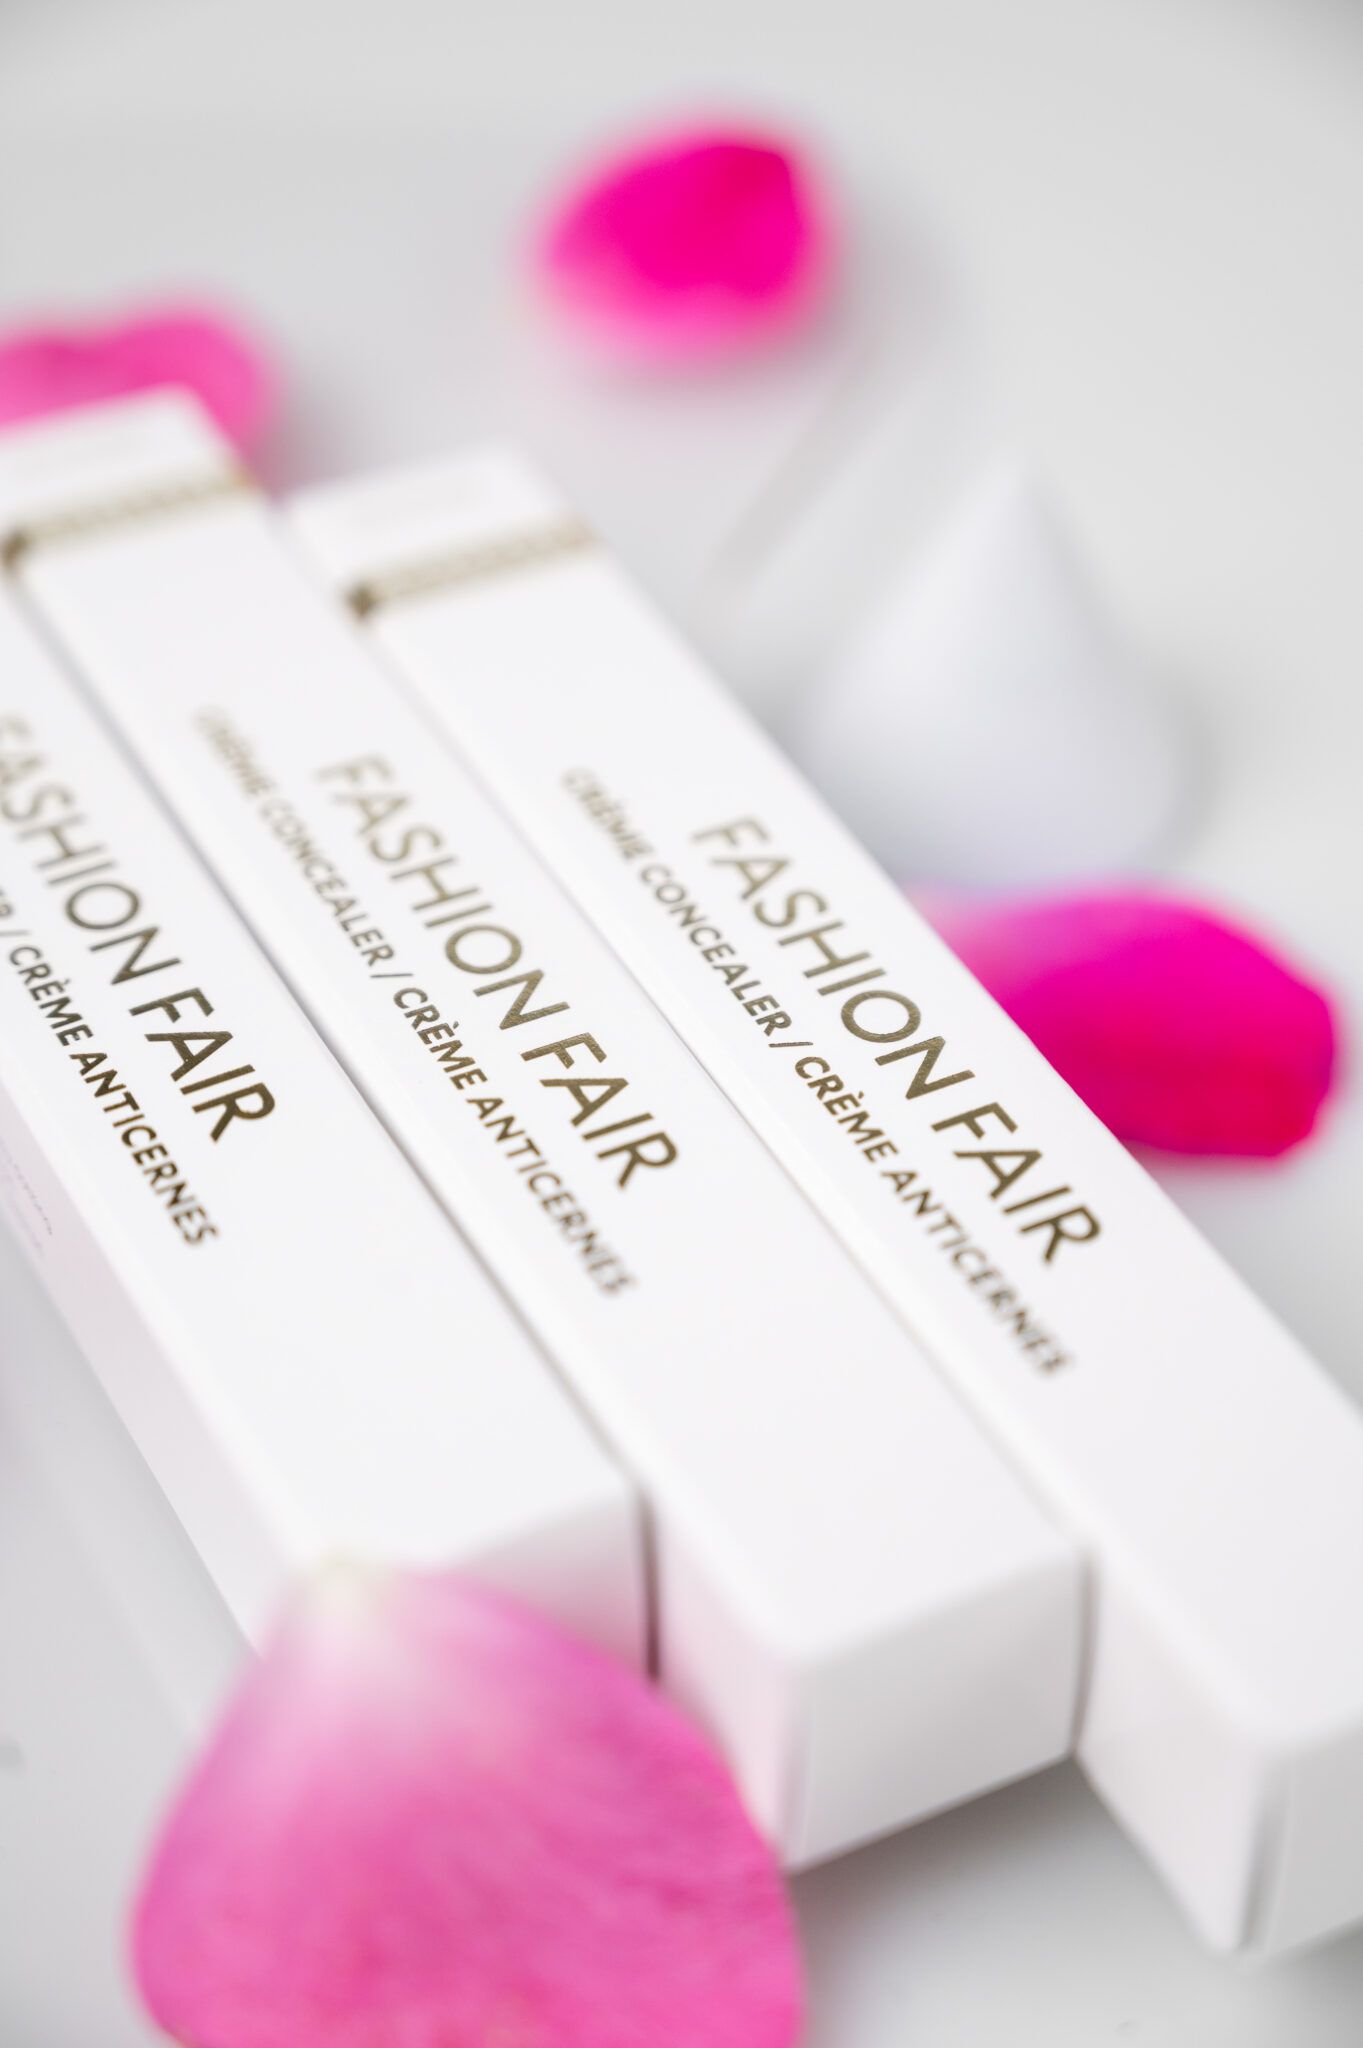
Hot stamping transfers a metallic or pigmented foil with heat and pressure, which is why it reads as premium. It also has hard limits.
- Minimum feature size. Very fine lines, small type and delicate detail may not transfer cleanly. Specify a minimum line weight and type size with the decorator.
- Curves. Foil struggles with fine detail on curved or compound surfaces, because pressure is uneven across the stamp area. Flat or gently curved panels give more reliable results.
- Material compatibility. The substrate, any coating beneath it and the foil have to suit one another. A foil that bonds well to one plastic may not bond to another.
Treat foil as a design feature to be sampled, not a finish you can assume. A sample on the production substrate tells you more than any drawing.
Soft-touch and matte: how they change everything else
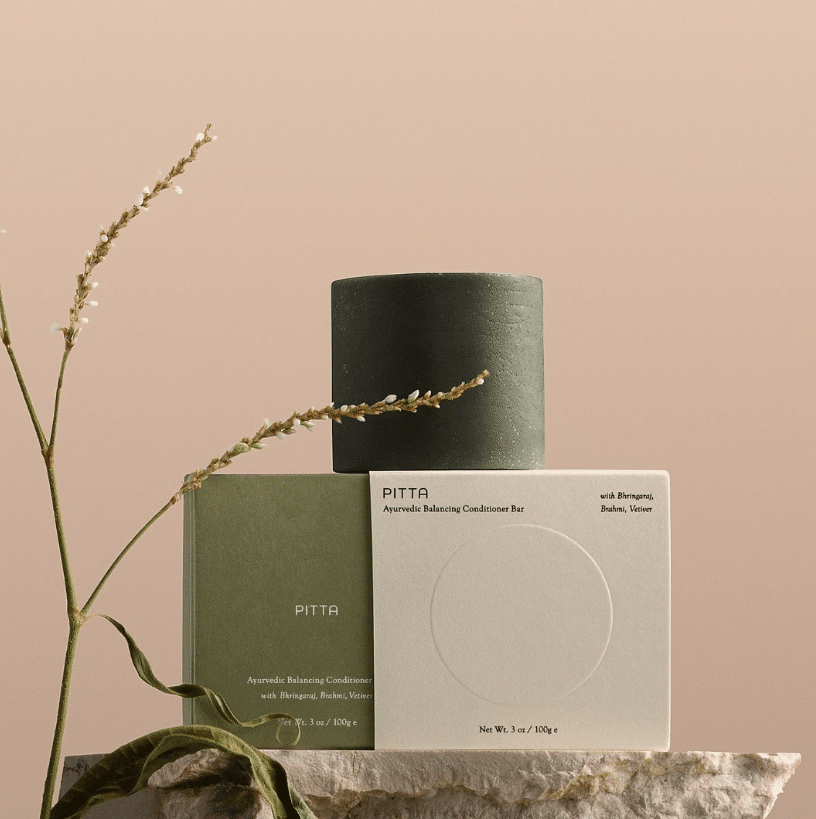
Soft-touch and matte coatings change the feel and look of a pack, and they also change how it behaves with other components.
- Label adhesion. A coated surface can be harder for adhesive labels to grip. Test the actual label and adhesive on the actual finish.
- Scuffing. Matte and soft-touch surfaces can show rub marks and burnishing from handling and from transit vibration. Cartons rubbing against each other in shipment can leave a visible mark.
- Consistency. Large flat areas of colour show variation more than textured or busy artwork, so shade and gloss tolerances need an agreed reference.
Because transit is a real source of surface damage, check the finish against the distribution test your pack will meet. ISTA's general simulation procedures combine shaped random vibration, drops and atmospheric conditioning, which is the kind of exposure that shows up a scuff-prone coating before a customer does.
Wrap and sleeve labels: shape matters
Wrap and shrink sleeve labels give excellent coverage and graphics, but they behave differently on tapered and straight-walled containers.
- Straight walls are the easiest case: the label sits flat and the artwork stays square.
- Tapered containers can cause sleeves to ride up, wrinkle or distort artwork unless the sleeve is designed and sized for the taper.
- Seams and registration. Where the seam falls, and how artwork is positioned relative to it, should be decided in the spec, not left to the applicator.
If you are weighing label options for a new container, our packaging selector can help narrow format choices before decoration is locked.
Assembly reality: decoration meets the line
A finish does not live on its own. It has to survive filling, capping, labelling, case packing and transport.
- Handling at speed. Check how decorated pieces are conveyed, orientated and capped. Contact points can mark soft or fresh finishes.
- Assembly stack-up. When a decorated body, a decorated closure and a label meet, small tolerances add up. Confirm alignment of logos, seams and panels on the assembled pack.
- Change control. ISTA's guidance is that tests should be repeated whenever there is a change to the product, package or process, including materials. A new coating, ink or supplier is a reason to re-check the finish.
These are the points where a co-man's input pays off. Your packaging might look great; your co-man might not be able to run it explains how to get that input early.
A decoration feasibility checklist
Before artwork is final, confirm the following in writing:
- The decoration method and the production line that will run it.
- Registration tolerance at production speed, not sample speed.
- Minimum line weight and type size for each method used.
- The behaviour of the finish with the label, adhesive and closure it will meet.
- How the finish holds through case packing and the distribution test you plan to run.
- A signed-off sample on the production substrate that becomes the reference for QC.
Put these into the spec using the spec clarity template, so a supplier is never left to guess. Order free samples of candidate components to see finishes in hand before you commit.
Read Looks Great, Fails in Production, or ask for our packaging process overview.
Frequently asked questions
What are the limits of silk-screen printing on cosmetic packaging?
Silk-screen needs cure time before pieces are handled or packed, and it holds a registration tolerance that gets more expensive as it tightens. Artwork near seams, shoulders or curves is harder to keep consistent. Ask the decorator for a written registration tolerance at production speed, and design artwork that survives small shifts.
Can hot stamping and foil be used on curved packaging?
Yes, but with care. Foil has a minimum feature size, and fine lines or small type may not transfer cleanly. On curved or compound surfaces pressure is uneven, so detail suffers. Flat or gently curved panels are more reliable. Always sample on the production substrate, because foil bonding depends on the material and any coating beneath it.
Do soft-touch and matte finishes affect labels?
They can. A coated surface may be harder for an adhesive label to grip, so test the actual label and adhesive on the actual finish. These finishes can also show rub marks and burnishing from handling and transit vibration, and large flat colour areas reveal shade variation more readily than busy artwork.
When should I check decoration feasibility for my packaging?
Before artwork is finalised. Confirm the decoration method, the production line that will run it, registration tolerance at production speed, minimum line weight and type size, and how the finish behaves with labels, closures and case packing. Doing this early costs a conversation, while finding limits after sampling can cost several rounds.
Do sleeve labels work on tapered containers?
They can, but a sleeve sized for a straight-walled container may ride up, wrinkle or distort artwork on a taper. The sleeve needs to be designed and sized for the actual container shape, and the seam position and artwork registration should be set in the spec rather than left to the applicator.
James Ford is the founder and CEO of Knockout Packaging Solutions. He works across primary and secondary packaging, sustainable and conventional, for beauty, health and wellness, and lifestyle brands, from sourcing and design through to logistics.
Last reviewed November 18, 2026. LinkedIn
Sources
- ISTA Test Procedures, International Safe Transit Association (ISTA)
- Getting Started with Design & Testing, International Safe Transit Association (ISTA)